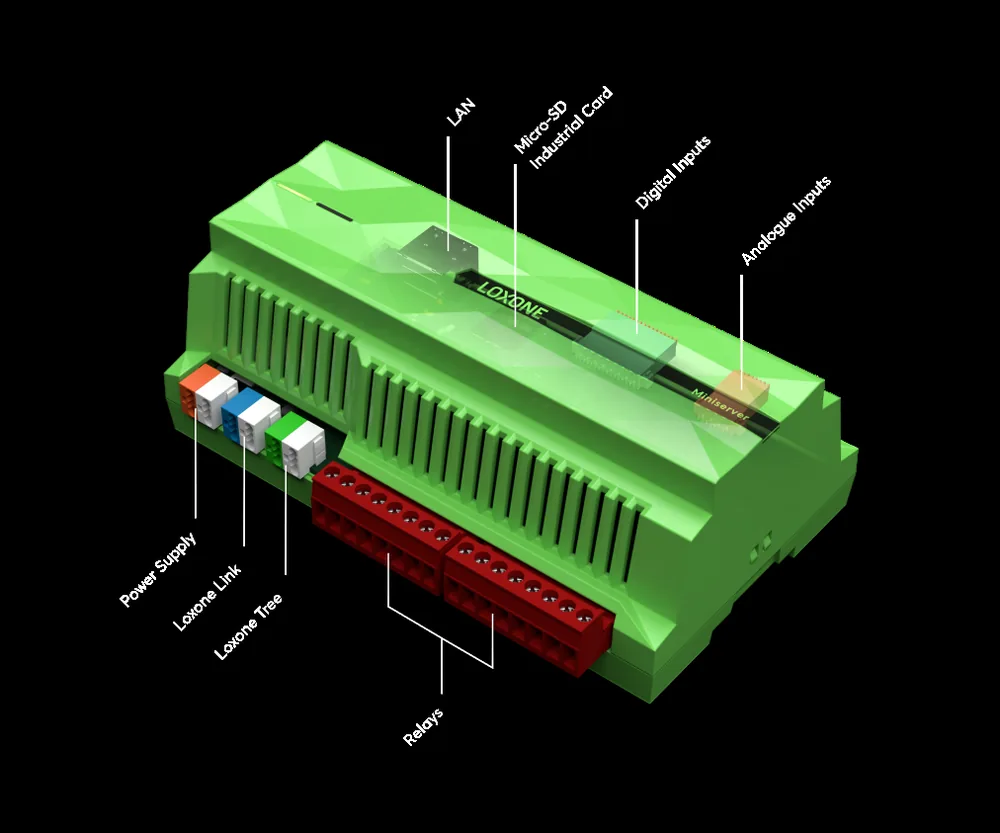
OEM & ODM
OEM & ODM for Building Automation
Control cabinets, custom panels, documentation, factory acceptance testing and project-specific engineering for building automation suppliers and integrators.
What OEM and ODM cover
OEM and ODM are often used as one term, but the boundary matters. OEM usually means we build to your design, brand and specification. ODM means we take more of the design responsibility for a product or panel family that you place on the market. In building automation, both models usually include control cabinet assembly, panel fabrication, custom interface panels, device mounting, wiring, labelling, documentation, factory acceptance testing and packaging. The commercial model should be agreed before the first drawing, not after the first prototype. The engineering boundary matters just as much: who owns the schematic, who approves a change and who signs the test record. A clear boundary prevents the most common dispute: a panel that meets the drawing but not the performance the buyer expected. Write the scope in deliverables, not in adjectives, and list what is excluded as carefully as what is included. A written scope also makes the quotation comparable between suppliers.
- Control cabinet assembly and wiring
- Custom panels and interface plates
- Device mounting and labelling
- Documentation, testing and packaging
From drawing to cabinet
A cabinet starts with a schematic, a bill of materials and a terminal plan. The production sequence is straightforward but unforgiving: cut and mount the enclosure, fit DIN rail and ducting, mount devices, wire to the drawing, label every conductor, test continuity and insulation, then apply power in stages. Layout should leave room for heat, cable bends and future additions. A cabinet that is tight on day one is a maintenance problem on day two. The build record should show who wired which panel, which drawing revision was used and what was changed. A production line that relies on memory instead of a drawing will produce a different cabinet every time. Keep mains and extra-low-voltage wiring separated, and respect the clearance the devices require. Use ferrules, torque settings and labelling consistently; those details decide whether a fault can be found. Photograph the interior before the doors close. A drawing that cannot be built should be corrected before production, not explained afterwards.
- Schematic, BOM and terminal plan
- Enclosure layout, heat and cable routing
- Wiring to drawing and conductor labelling
- Continuity, insulation and staged power-up
Custom panels and project-specific engineering
Not every project fits a catalogue panel. A hotel floor may need a room-control panel with keypad interfaces; a plant room may need a mixed mains and extra-low-voltage cabinet; a retrofit may need a panel that fits an existing recess. Project-specific engineering covers the interface between the building services design and the panel: point schedules, terminal allocation, signal types, segregation, surge protection and access for maintenance. We work from the consultant's or contractor's design and flag conflicts before production, not during installation. Where the design is incomplete, the gap should be named and agreed, not filled silently on the shop floor. A design review before release is cheaper than a rework after assembly. The review should check terminal capacity, heat load, cable entries and door swing, not only the circuit logic. It should also check that the panel can be maintained without removing the whole enclosure. The review should record every deviation and who approved it.
- Room, floor and plant-room panels
- Mixed mains and extra-low-voltage layouts
- Retrofit and recessed panel formats
- Point schedule and terminal allocation
Documentation and factory acceptance testing
Documentation is part of the product. A useful pack includes as-built schematics, panel layout, bill of materials, terminal list, device list, labelling schedule, test records and the configuration backup. Factory acceptance testing checks the panel before it ships: power distribution, I/O mapping, signal simulation, alarm behaviour and communication to the controllers. The test should follow a written procedure with expected results, and the customer should witness or receive the record. A panel that leaves the workshop untested moves the defect to the site, where it costs more. The FAT record should name the drawing revision, the firmware and the configuration that were tested. Test the signals at the terminals, not only in the software. Test the loss of power and the return of power, because that is when sequence faults appear. Test the communication path to every controller in the panel. A signed record is more useful than a photo of a screen. Test records should be traceable to the panel serial number and the project.
- As-built schematics and panel layout
- BOM, terminal list and labelling schedule
- I/O simulation and communication test
- Witnessed FAT and signed record
Packaging, logistics and handover
Packaging should protect the panel, not just contain it. Internal bracing, terminal covers, desiccant where needed, edge protection and clear labelling by panel and floor reduce damage and site confusion. Spare terminals, fuses and labels should be packed with the panel, not ordered later. The shipping list should match the BOM and the panel schedule. On arrival, the receiving team needs a packing list, a damage-check procedure and a contact for missing items. Handover is complete when the documentation, the test record and the physical panel agree. A panel that arrives with the right hardware and the wrong drawing is not delivered. Label the outside of the package with the panel ID, the floor and the project, not only the address. Keep a photo of the packed panel and the shipping list in the project record. Agree who pays for transport damage and who files the claim before the first shipment. A clear packing list reduces the site time spent searching for parts.
- Internal bracing and terminal protection
- Panel, floor and project labelling
- Spares, fuses and labels packed together
- Packing list and damage-check procedure
Responsibilities, change control and after-sales
Most OEM disputes are boundary disputes. The buyer owns the design intent, the brand and the market approval; the builder owns the workmanship, the drawing compliance and the test record. Component warranties sit with the component supplier, and the panel warranty sits with whoever assembled it. Those lines should be written before production. Change control should use a revised drawing and a change log; undocumented changes make the as-built pack inaccurate. After-sales support should define the spare-parts policy, the response path and the person who can approve a replacement. A clear boundary is not a legal formality; it is what makes a repeat order possible. Do not promise an approval that is not in the agreed scope, and do not imply a scale or capability that has not been verified. State what is known and what is not. A repeat order is easier when the boundary and the records are stable.
- Buyer owns design intent and market approval
- Builder owns workmanship and drawing compliance
- Change log with revised drawings
- Spare-parts and response path defined
OEM and ODM scope
14 rows| Scope | Typical input | Deliverable |
|---|---|---|
| Design review | Drawing set, point schedule, project standards | Reviewed design and comment log |
| Component sourcing | Approved maker list and alternatives | Sourced BOM and lead times |
| Enclosure and layout | Enclosure specification, heat load, cable entries | Laid-out cabinet |
| Control cabinet assembly | Schematic, BOM, terminal plan | Wired and labelled cabinet |
| Panel fabrication | Panel drawing, cut-outs, finish | Custom panel and interface plate |
| Device mounting | Device list and layout | Mounted and labelled devices |
| Wiring and termination | Terminal plan, cable schedule | Terminated and tested wiring |
| Labelling | Naming convention and panel schedule | Conductor, device and panel labels |
| Documentation | Drawing set and project standards | As-built pack and test records |
| Factory acceptance test | Test procedure and witness plan | Signed FAT record |
| Configuration backup | Controller programme and settings | Versioned backup |
| Packaging and logistics | Shipping list and site sequence | Protected, labelled packages |
| Spares and consumables | Maintenance policy | Spares kit and label set |
| Change control | Change request and drawing revision | Revised drawing and change log |
Project images
3 images
Frequently asked
01Do you build to our drawings or design the panel?
Both models are possible. OEM work usually follows your drawings and specification; ODM work can include the panel design, component selection and documentation. The boundary should be written into the contract before production.
02What documentation comes with a panel?
Typically as-built schematics, panel layout, bill of materials, terminal list, device list, labelling schedule, test records and configuration backup. The exact pack is agreed at the start, because it affects production time.
03What is FAT and do we need it?
Factory acceptance testing checks the panel before shipment: power, I/O mapping, signals, alarms and communication. It is useful on any project where site access is restricted or rework is expensive. The test follows an agreed procedure and produces a signed record.
04Can you handle small batches or one-off panels?
The production model should match the project. One-off and repeat panels use different documentation and testing routines, and the quotation should state which is included.
05Do you supply the controllers and devices?
Components can be sourced to the project specification or supplied by you. The commercial and warranty responsibility for each item should be stated in the contract, especially where branded products are involved.
06Can you private-label a panel for our brand?
Yes, where the component suppliers' terms allow it and the brand and documentation responsibilities are agreed. Private labelling does not transfer product approval or regulatory responsibility automatically.
07What standards do you build to?
The standards named in the project specification and the applicable local electrical rules. We do not claim approvals that are not part of the agreed scope. The verification and approval responsibility should be explicit in the contract.
08How do you handle changes after the drawing is approved?
With a change log and a revised drawing revision. Production should not absorb undocumented changes; every deviation needs an owner and a record, or the as-built documentation stops matching the panel.
Next step
Bring us the building.
Tell us the building type, systems in scope and the outcome you need. We will map the shortest path to a working system.